

 Rings
 Earrings
 Bracelets & Bangles
 Necklaces & Pendants
 Silver Jewellery


 Our Story
 Diamond Buying Guide
 Watch Buying Guide
 Product Care & Aftercare
 Visit our Showroom
Production, Design, and Sustainability in 18ct Gold Jewellery: Casting, Finishing, and Ethical Sourcing of Alloys
When you hold a piece of masterfully crafted fine jewellery, there is an immediate sensation of warmth, weight, and presence that is impossible to fake. For centuries, goldsmiths have considered 750 parts per thousand—famously known as 18 karat—to be the absolute golden ratio of fine jewellery making. It holds three-quarters pure elemental gold by mass, delivering that unmistakable rich glow, while the remaining quarter consists of carefully balanced metals that provide real-world durability. Transforming raw elemental grain into exquisite 18ct gold jewellery requires an intricate balance between artistic intuition, precise metallurgical chemistry, and modern engineering. Today, that narrative also demands an uncompromising commitment to ethical sourcing and environmental stewardship.
Every ring, pendant, or bracelet that leaves a traditional jeweller’s bench tells a silent story of transformation. Molten liquid metal cools into complex crystalline matrixes; precision cutting tools slice away micro-shavings to reveal mirror facets; and skilled gem-setters manipulate tiny metal claws with surgical accuracy. Understanding how this material travels from responsible mines and closed-loop refineries through the casting ovens and onto the jeweller’s bench reveals why 18ct gold remains the benchmark of modern luxury.
From Digital Blueprint to Physical Master: Design and Prototyping
Before any gold is melted, a design must find its structural footing. Historically, jewellery design relied entirely on hand-carved wax blocks or directly forged metal models. While traditional hand fabrication remains revered for bespoke, one-off masterpieces, the modern fine jewellery workshop relies heavily on advanced Computer-Aided Design (CAD). Specialised jewellery software allows designers to calculate metal volumes, structural load-bearing tolerances, shrinkage ratios, and exact gem clearances down to hundredths of a millimetre.
Designing for 18ct gold requires a keen understanding of the metal's physical behaviour. Because 18ct gold is significantly denser than silver or lower-karat golds (averaging between 15.1 and 15.9 grams per cubic centimetre depending on the specific alloy), a piece must be engineered to balance luxurious heft with day-to-day comfort. Wall thicknesses must be meticulously mapped; if a ring shank is hollowed out too aggressively to save weight, it risks structural deformation under everyday strain. Conversely, solid cross-sections must allow for proper metal flow during casting to avoid cold shuts or air pockets.
Once a digital design is perfected, high-resolution 3D printers transform the digital render into a physical reality using photopolymer castable resins or specialised carving waxes. These printed models capture microscopic details, from micro-pavé seats to delicate filigree openwork. They serve as the sacrificial heart of the lost-wax casting method—a manufacturing discipline that dates back more than five thousand years, now refined with aerospace-grade precision.
The Lost-Wax Investment Casting Cycle
Lost-wax casting, or investment casting, is the primary method used to produce intricate 18ct gold jewellery components. It is a process that is both brutal and delicate, exposing materials to extreme thermal transitions while maintaining microscopic fidelity.
The journey begins with the creation of a "tree." Multiple wax or resin prototypes are attached via individual pathways, known as sprues, to a central wax trunk. The arrangement of these pieces is an art in itself: heavier items sit closer to the base or main reservoir, while lighter components branch outward, ensuring that molten gold can flow freely and solidify evenly without starving any section of the tree.
| Stage | Process Details | Critical Quality Control Factors |
|---|---|---|
| Investing | The wax tree is suspended inside a steel flask and submerged in a liquid refractory plaster slurry (gypsum-bonded investment). | Vacuum degassing to remove every micro-bubble from the slurry before it cures. |
| Burnout Cycle | The cured flask is transferred to a computer-controlled kiln, gradually heated from 150°C to roughly 730°C over 10 to 14 hours. | Complete elimination of wax and resin residue without cracking or degrading the internal gypsum cavity. |
| Induction Melting | 18ct gold alloy casting grain is melted inside a graphite crucible using high-frequency electromagnetic induction. | Strict temperature regulation (typically 1000°C–1100°C) under an inert argon gas blanket to prevent oxidisation. |
| Pour & Solidification | Liquid gold is drawn into the hollowed flask using positive pressure or vacuum-assisted draw. | Controlled directional cooling to prevent shrinkage porosity and promote a dense, fine crystal grain. |
When the molten gold enters the red-hot flask, it immediately begins to cool and solidify against the investment walls. If the flask cools too quickly, the metal can suffer from thermal shock, developing internal stress fractures. If it cools too slowly, excessive crystal grain growth can occur, leaving the gold brittle and prone to surface pitting. Once the metal has dropped below its recrystallisation temperature, the glowing flask is quenched in water. The thermal shock causes the investment plaster to violently fracture and disintegrate, emerging to reveal a gleaming, golden tree bearing dozens of raw jewellery castings.
Microstructure, Annealing, and Work Hardening
Freshly cast 18ct gold possesses an as-cast dendritic microstructure. Although fully functional, cast gold often exhibits slightly lower mechanical strength than metal that has been wrought, rolled, or drawn through a die. For items that must endure intense daily mechanical stresses, such as wedding rings, tennis bracelet clasps, and earring posts, cold working and controlled heat treatment are essential.
Cold working—such as forging with a hammer, rolling through steel mills, or die-striking—mechanically deforms the gold's crystal lattice. As dislocations within the atomic planes pile up and entangle, the alloy undergoes work hardening. Its yield strength and Vickers hardness (HV) increase substantially. However, excessive cold working makes the metal brittle. If worked past its physical limits, micro-fractures develop along the grain boundaries, eventually causing the piece to crack clean through.
To restore workability, goldsmiths utilise annealing. The piece is carefully brought to a specific annealing temperature (typically between 600°C and 680°C depending on whether the alloy is yellow, white, or rose), held at that temperature briefly, and then quenched or allowed to cool in a controlled atmosphere. This thermal reset triggers recrystallisation: new, strain-free grains nucleate and grow throughout the matrix, restoring the metal’s native ductility without compromising its structural integrity. Understanding how these mechanical treatments interact with different alloy compositions—such as copper-heavy rose gold versus nickel-free palladium white gold—is explored in depth throughout our analysis of 18ct gold colour variants.
The Bench Craftsman’s Touch: Fettling, Assembly, and Stone Setting
While casting and metallurgy provide the raw form, it is the manual bench work that elevates a rough gold casting into a fine piece of jewellery. Once the individual pieces are clipped from the casting tree, they enter the fettling and finishing phase.
First, the goldsmith removes the casting sprue using fine hand saws and coarse files, meticulously levelling the contact point until it seamlessly merges with the contour of the design. Next, magnetic pin tumblers, emery paper sticks, and micro-motor rotary burrs are employed in sequence. Each abrasive step systematically replaces larger surface scratches with increasingly microscopic ones, progressing from 240-grit through to 1200-grit silicon carbide abrasives.
If the jewellery consists of multiple components—such as a ring requiring a separate head to house a central diamond, or a bracelet made from articulated links—the craftsman joins them using 18ct gold solder. Solder is an alloy intentionally formulated with a slightly lower melting point than the jewellery itself, achieved by altering the ratio of silver, copper, and zinc. Goldsmiths work through a descending temperature ladder (Hard, Medium, and Easy solders), ensuring that subsequent joints can be soldered without accidentally melting the joints made previously.
Precision Stone Setting
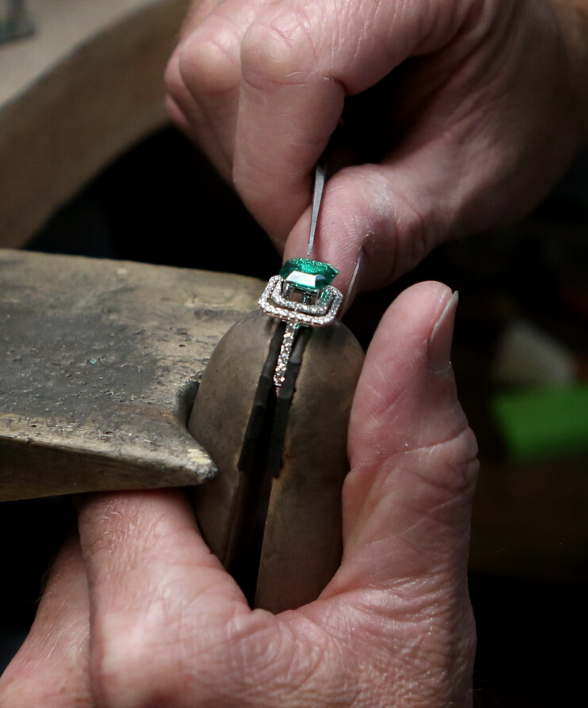
Setting gemstones into 18ct gold is one of the most demanding disciplines in the trade. The metal must be ductile enough to fold smoothly over the girdle of a precious stone without springing back, yet rigid enough to hold that gem firmly in place through decades of daily wear. Goldsmiths use specialised steel tools called gravers to cut bright, reflective borders, carve delicate beads, or raise secure prongs:
- Claw or Prong Setting: Small pillars of gold are notched precisely to fit the gem's pavilion and girdle, then pushed gently over the crown facets and rounded with cup burrs to create smooth, snag-free tips.
- Bezel Setting: A continuous collar of 18ct gold is pushed inward around the entire perimeter of the gem using a burnisher or punch, locking the stone into a protective, modern frame.
- Pavé Setting: Tiny holes are drilled closely together into the gold surface. The setter raises microscopic beads of gold directly from the plate using razor-sharp chisels, securing a continuous field of diamonds that looks like a glittering, paved street.
- Channel Setting: Stones are suspended side-by-side between two parallel walls of gold, offering clean, geometric lines that safeguard the stones' fragile edges from impact.
The High-Lustre Finish and Electroplating
Once stone setting is complete, the piece moves to the polishing lathe. High-speed mops impregnated with abrasive compounds, such as tripoli, cut away the final traces of surface imperfection. This is followed by a secondary buffing with fine jeweller’s rouge (iron oxide) or specialised diamond pastes, which gently burnishes the surface to a mirror-like, liquid shine.
For 18ct white gold, the finishing process often includes an electroplated layer of rhodium—a rare, ultra-white platinum-group metal. While premium 18ct white gold alloyed with high levels of palladium features an attractive warm-grey tone naturally, rhodium plating provides an icy, mirror-bright surface that provides temporary scratch resistance and enhances diamond fire. Over time, this plating gently wears away in high-friction areas, serving as an honest reminder of the ring's journey and prompting straightforward re-finishing during regular maintenance.
Sustainability and Ethical Sourcing of Alloys
In modern fine jewellery manufacture, how a piece is made matters just as much as its aesthetic beauty. Gold mining carries a significant social and environmental footprint. Historically, artisanal and industrial gold extraction has raised real concerns regarding mercury and cyanide use, soil erosion, carbon emissions, and poor labour conditions. As a result, the fine jewellery landscape has fundamentally shifted towards transparent, ethical supply chains.
Circular Metallurgy: The Power of Recycled Gold
Gold is infinitely recyclable. An atom of gold mined five thousand years ago in ancient Nubia can be melted down, refined back to pure 99.99% gold, re-alloyed to 18ct standards, and set into a modern engagement ring without any loss of quality, structural performance, or brilliance. Unlike plastics or paper, gold never degrades through recycling.
Modern workshops actively implement closed-loop manufacturing systems. Every milligram of gold generated during the creation process is captured:
- Bench Sweeps and Filing Trimmings: Jewellers work over leather skins or shallow bench drawers that catch cut-off sprues, wire ends, and coarse filings.
- Polishing Dust Filtration: Industrial dust-extraction systems pull the microscopic particles shed during mechanical polishing through high-efficiency particulate air (HEPA) filters, recovering valuable gold dust that would otherwise be lost.
- Wash Basin Settling Tanks: Even the water used to wash jewellers' hands and rinse ultrasonic cleaning baths is routed through specialized settlement traps to extract trace sediment.
When collected, this material is sent to certified precious metal refiners who use electrochemical processes (such as the Wohlwill process) or chemical aqua regia refining to separate pure gold from base metals, copper, and silver. The recovered 24-karat gold is then blended with virgin or certified recycled master alloys to produce fresh, high-grade 18ct casting grain that carries a dramatically lower environmental footprint than freshly mined metal.
Fairtrade and Fairmined Gold
While recycled gold plays a crucial role in reducing environmental impact, completely abandoning mined gold would cut off millions of artisanal miners from their primary livelihood. This is where initiatives like Fairtrade Gold and Fairmined Gold step in. These independent certifications focus on Artisanal and Small-scale Mining (ASM) organisations, transforming how gold is extracted at the grassroots level.
Certified artisanal cooperatives agree to strict environmental requirements: eliminating toxic mercury and cyanide wherever possible, restoring worked landscapes, and protecting local water sources from chemical runoff. In return, miners receive a guaranteed fair minimum price for their gold alongside an additional financial bonus—the Fairtrade or Fairmined Premium. Mining communities invest these funds directly into essential local infrastructure, such as clean water systems, schools, medical facilities, and safer mining machinery.
For independent British jewellers committed to accountability, such as Finnies the Jeweller, integrating certified traceable gold or fully audited recycled materials forms the cornerstone of responsible luxury. Discerning buyers can wear their pieces with genuine pride, confident that their jewellery uplifts communities while safeguarding delicate natural ecosystems.
Ensuring Authenticity: Hallmarking and Responsible Practice
Every effort invested in sourcing, casting, hand-finishing, and stone setting culminates in a final, legally binding seal of approval: the hallmark. In the United Kingdom, statutory hallmarking dates back to the fourteenth century, providing buyers with an independent guarantee of precious metal purity. Unlike some countries where jewellers simply stamp their own pieces, UK law requires that every article sold as 18ct gold must undergo rigorous assaying by an independent Assay Office in London, Birmingham, Sheffield, or Edinburgh.
Assayers sample the metal using precise methods, such as X-ray fluorescence spectrometry or traditional fire assay (cupellation), to verify that the piece meets the strict minimum standard of 750 parts per thousand pure gold. Once verified, the piece is stamped or laser-engraved with the sponsor’s maker mark, the fineness mark (750), and the official Assay Office town mark. This centuries-old consumer protection mechanism confirms that the artistry on the outside is matched by genuine integrity on the inside.
Caring for 18ct Gold: Preserving Value and Craft for Generations
Because 18ct gold contains 25% noble and functional alloying metals, it strikes a wonderful balance: it resists tarnishing and corrosion far better than 9ct or 14ct gold, while resisting everyday denting and abrasive wear far better than pure 22ct or 24ct gold. However, like any fine luxury material, it still deserves thoughtful care to maintain its radiant finish.
Chlorine is the greatest chemical enemy of gold alloys. While pure gold is completely inert to chlorine, the copper, nickel, or zinc present in 18ct alloys will react with chlorinated pool water, hot tubs, and household cleaning bleach. Over prolonged exposure, chlorine triggers stress corrosion cracking along internal grain boundaries, weakening delicate prongs and leading to lost gemstones. Removing jewellery before swimming or cleaning is an easy way to prevent irreversible structural damage.
Regular maintenance at home is wonderfully straightforward. A short soak in warm water with a few drops of mild washing-up liquid, followed by a gentle scrub with a soft-bristled baby toothbrush, will dissolve natural skin oils, lotions, and dust that collect beneath stone settings. Periodic visits to your jeweller allow for professional ultrasonic cleaning, steam cleaning, prong inspection, and light buffing, ensuring your fine 18ct jewellery will be passed down, cherished, and admired for generations to come.